Business Details
Trusted Industrial Flooring & Refractory Solutions
Ancorite Surface Protection is a leading provider of industrial flooring systems, refractory linings, and anti-corrosive solutions with decades of experience serving diverse sectors. As part of the Steuler Group, we combine global expertise with local execution to deliver tailored, high-performance systems for demanding environments. Our services span resin flooring, terrazzo installations, ceramic tiling, and GRP pipework, supported by a commitment to innovation and technical excellence. With operations across the UK, Ireland, and internationally, we prioritise rapid mobilisation, durability, and client collaboration.Our team of specialists ensures projects meet rigorous safety and quality standards, from small repairs to large-scale turnkey contracts. Backed by advanced materials and a holistic approach, we address challenges in chemical resistance, hygiene, and structural resilience. Trusted by multinational clients like BP and Diageo, we maintain a proven track record in sectors including pharmaceuticals, food and beverage, and energy. Our vision focuses on long-term partnerships, sustainability, and exceeding industry benchmarks through continuous improvement.
Services
Resin Flooring
Terrazzo Flooring
Ceramic Tiling
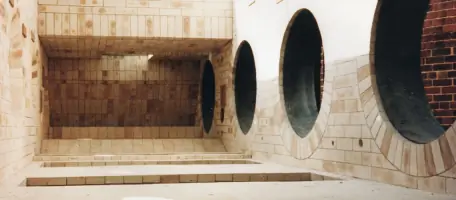
Refractory Linings
GRP Pipework
Highlights and features
- We offer tailored flooring and lining solutions for industries including pharmaceuticals and energy.
- Our team has decades of experience in extreme chemical and thermal environments.
- We provide rapid mobilisation to minimise downtime for critical projects.
- We are part of the Steuler Group, ensuring access to global expertise and materials.
- Our installations meet ISO standards and client-specific safety requirements.
What people say
Exceptional quality
Professionalism and expertise
Seamless process
Outstanding workmanship
Meets safety standards
Services
Resin Flooring
Ancorite provides high-performance polyurethane and epoxy resin flooring systems designed for industrial and commercial environments. These solutions offer chemical resistance, durability, and hygienic finishes suitable for pharmaceutical, food processing, and power generation sectors. Our installations include anti-slip quartz aggregates and decorative quartz or flake epoxy systems, ensuring both functionality and aesthetic appeal.
Terrazzo Flooring
Our polyurethane and epoxy terrazzo systems combine durability with visual impact for commercial and pharmaceutical applications. Featuring anti-static properties and seamless finishes, these floors withstand aggressive solvents and frequent cleaning. Custom designs using glass, marble, or mirror glass elements are available for high-profile locations like shopping centres and healthcare facilities.
Refractory Linings
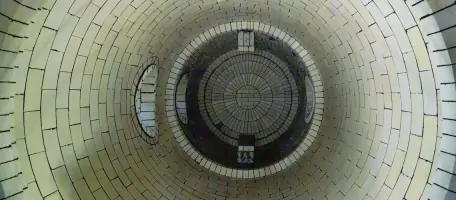
Ancorite specialises in refractory brickwork, castables, and ceramic fibre linings for extreme temperature environments. These systems protect industrial furnaces, incinerators, and chemical processing units. Our solutions include chromium oxide bricks, silicon carbide linings, and modular ceramic fibre installations, engineered to meet specific thermal and mechanical demands in steel, petrochemical, and energy sectors.
GRP Pipework
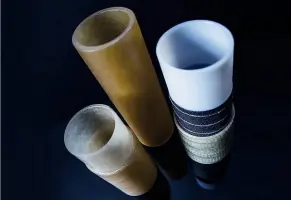
We install glass-reinforced plastic (GRP) and GRE pipework systems for aggressive chemical environments. These lightweight, durable solutions handle acid distribution, effluent treatment, and utility lines. Custom fabrication of bends, reducers, and flanges ensures compatibility with existing metal or thermoplastic systems, meeting ISO and client-specific standards.
Ceramic Tiling
Ancorite offers vibration, traditional, and corrosion-resistant ceramic tiling for food, pharmaceutical, and chemical industries. Our systems use vitrified tiles with epoxy or cementitious grouts to create impervious barriers against solvents and heavy traffic. Anti-static properties and secondary chemical-resistant membranes are incorporated for critical environments like clean rooms and brewing facilities.
Questions
What industries do Ancorite's flooring systems serve?
Our systems are tailored for pharmaceuticals, food and beverage, chemical, energy, and commercial sectors.
Can Ancorite handle international projects?
Yes, we support clients globally with turnkey solutions and localised execution.
What materials are used in refractory linings?
We use fireclay bricks, castables, ceramic fibre, and silicon carbide for high-temperature environments.
Do you provide maintenance for existing installations?
Yes, we offer planned and reactive maintenance for flooring, linings, and pipework systems.
How are projects managed from start to finish?
Our teams handle specification, installation, and quality assurance, ensuring compliance with ISO and client standards.
What accreditations does Ancorite hold?
As part of the Steuler Group, we adhere to global quality and safety benchmarks in all operations.